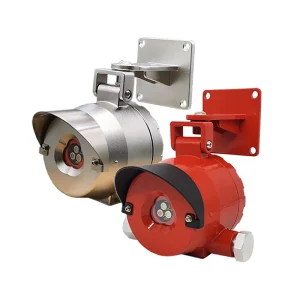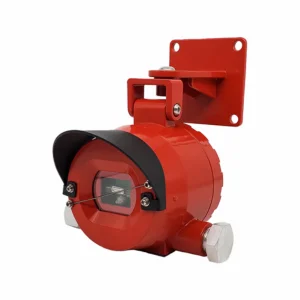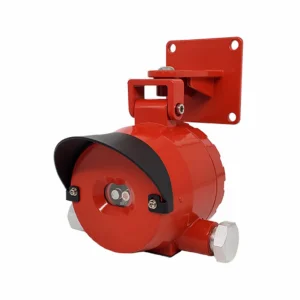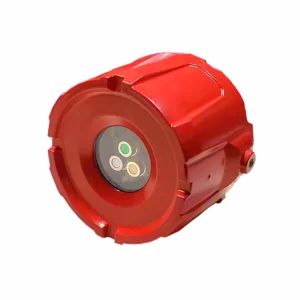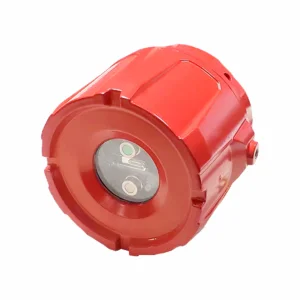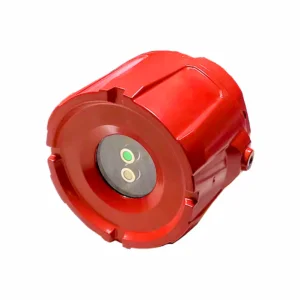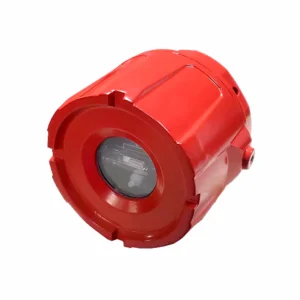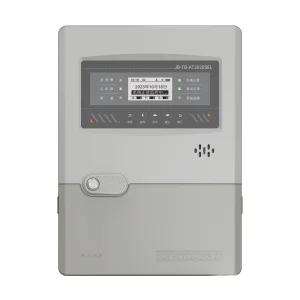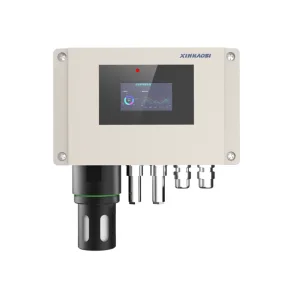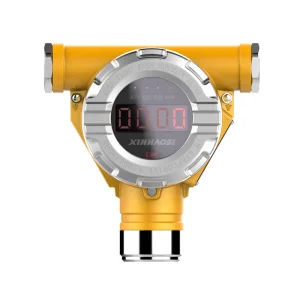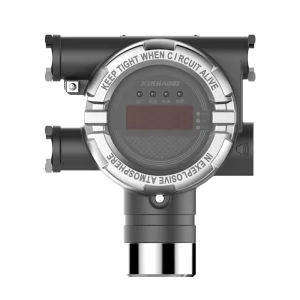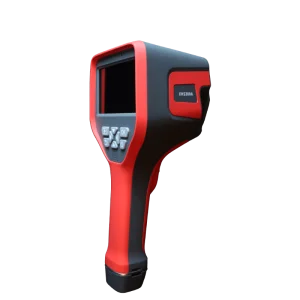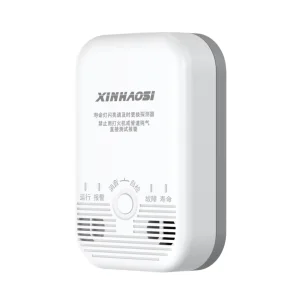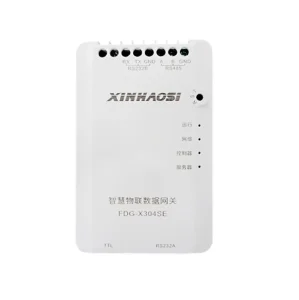
Engineered for high-reliability hazardous environment monitoring, featuring state-of-the-art multi-spectrum optical sensors designed for rigorous industrial deployments.
Strategic market analysis, localization compliance, and supply chain advantages bridging world-class Chinese manufacturing with Mbarara's dynamic economic sectors.
Mbarara, as a vital commercial and industrial hub in southwestern Uganda, is experiencing rapid commercial acceleration across agro-processing, light manufacturing, logistics storage, and regional fuel distribution networks. With this economic expansion comes an increased imperative for rigorous industrial safety standards. Facilities handling combustible materials, biomass boilers, petroleum storage terminals, and chemical warehouses require instantaneous, highly accurate optical fire detection systems to prevent catastrophic incidents.
Traditional thermal and smoke detectors often face severe limitations in expansive industrial settings due to slow response times or susceptibility to environmental dust. As a specialized flame detector manufacturer, our advanced multi-spectrum infrared (IR) and ultraviolet (UV) flame detectors are uniquely engineered to identify specific spectral signatures of hydrocarbon and non-hydrocarbon fires within milliseconds—even amidst high ambient temperatures and tropical climatic variations typical of the Mbarara region.
Leveraging our advanced manufacturing bases in Chengdu and Deyang, we operate fully integrated automated production lines equipped with surface-mount technology (SMT), automated optical inspection (AOI), and multi-chamber environmental testing facilities. This robust supply chain allows us to maintain strict quality control while offering highly competitive OEM/ODM pricing structures for international procurement agents, EPC contractors, and safety distributors serving Mbarara and the broader East African market.
Every flame detector and gas safety controller leaving our factory undergoes rigorous calibration and validation under ISO9001 and CNAS-accredited laboratory standards. This ensures uncompromised reliability, high immunity to false alarms caused by solar radiation, lightning, or artificial lighting, and long-term durability in challenging industrial environments.
Two decades of dedicated innovation in gas safety and optical flame detection technology.
Adhering strictly to international quality management frameworks, our core product series hold comprehensive certifications including CE, SIL, explosion-proof approvals, and CPA measurement instrument type approvals. Our in-house laboratory is accredited by the China National Accreditation Service for Conformity Assessment (CNAS) under the ILAC-MRA framework (ISO/IEC 17025), guaranteeing that every device supplied to the Mbarara market meets rigorous global safety benchmarks.
Our intelligent graphical monitoring systems integrate advanced predictive maintenance analytics based on historical operational data, reducing potential equipment failure rates by over 30% and providing total operational transparency for plant operators.
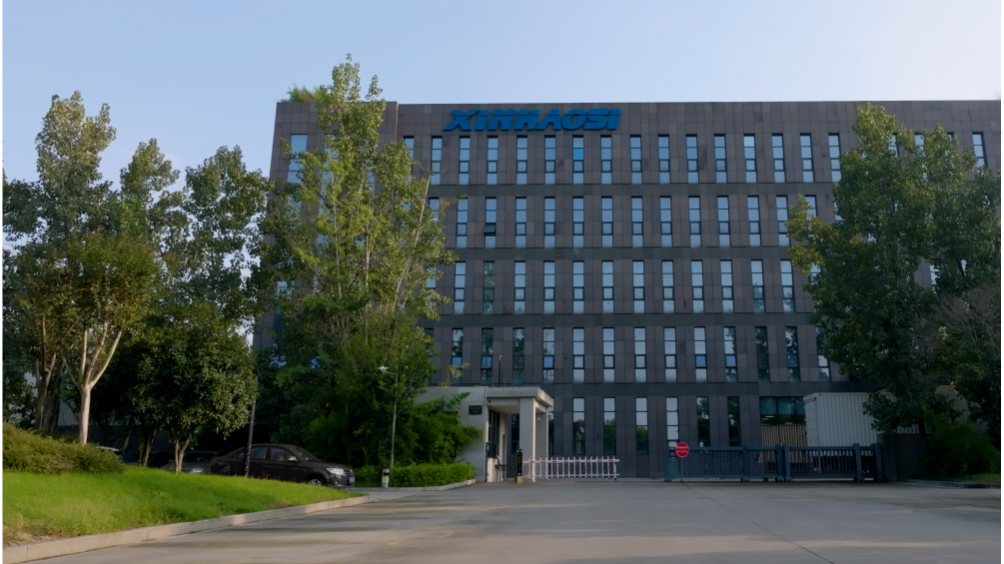
Serving as our global headquarters, integrating advanced R&D, international marketing, and executive management.
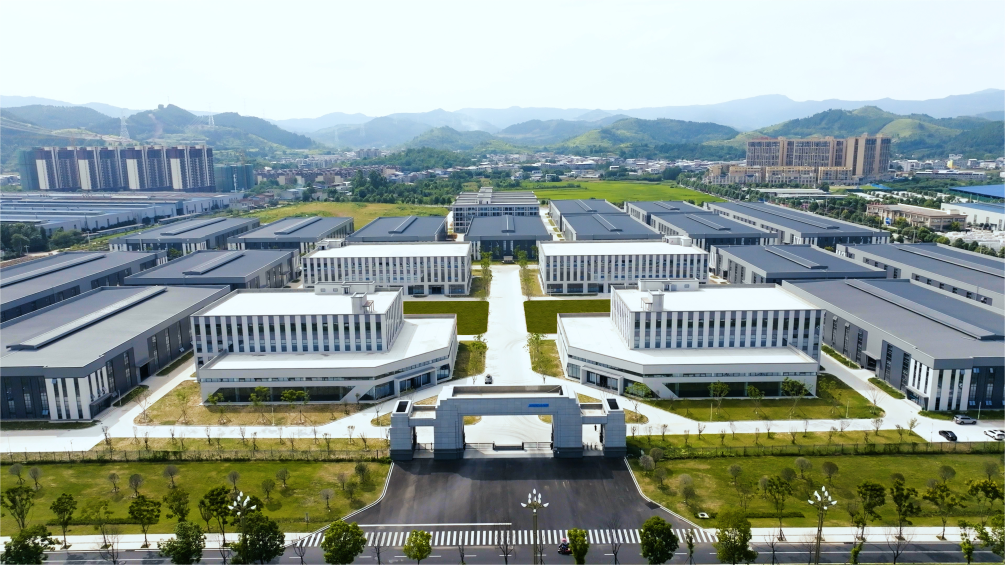
Our state-of-the-art intelligent manufacturing facility equipped with high-speed automated production lines and rigorous testing chambers.
Expert answers regarding flame detector selection, installation, and procurement for industrial applications in Mbarara.
Explore our full range of certified flame detectors, gas controllers, and smart monitoring equipment tailored for industrial safety infrastructure.
Chengdu Factory & Office
Deyang Factory
Founded in 2003, Xinhaosi is one of the most influential and trusted brands in the global gas safety industry. Over the past two decades, we have steadily built a robust and comprehensive production and service system, which integrates cutting-edge R&D, intelligent manufacturing with advanced automation equipment, digital marketing across global channels, professional after-sales support with an experienced technician team, flexible OEM/ODM services, as well as CNAS-Accredited laboratory calibration services that meet international standards.
Our diversified product portfolio covers industrial & residential gas detection & alarm systems, industrial & household gas solenoid valves, and urban gas pipeline network monitoring systems—all engineered to adapt to complex working environments and strict safety requirements. We produce and sell tens of millions of units annually, catering to a wide range of industries that demand reliable gas detection solutions, including oil & gas exploration and production, petrochemicals, urban gas distribution, automotive manufacturing, pharmaceuticals, new energy, steel production, and beverage processing.
Guided by the core mission of “Making Gas Safety Accessible Everywhere,” we consistently deliver high-performance, reliable products and customized solutions tailored to each client’s unique needs. Every item we manufacture undergoes rigorous quality control tests, and every service we provide is backed by our professional technical team, fully embodying our unwavering commitment to safeguarding gas safety across both industrial workplaces and residential environments, and striving to build a safer world with sustainable gas safety technologies.
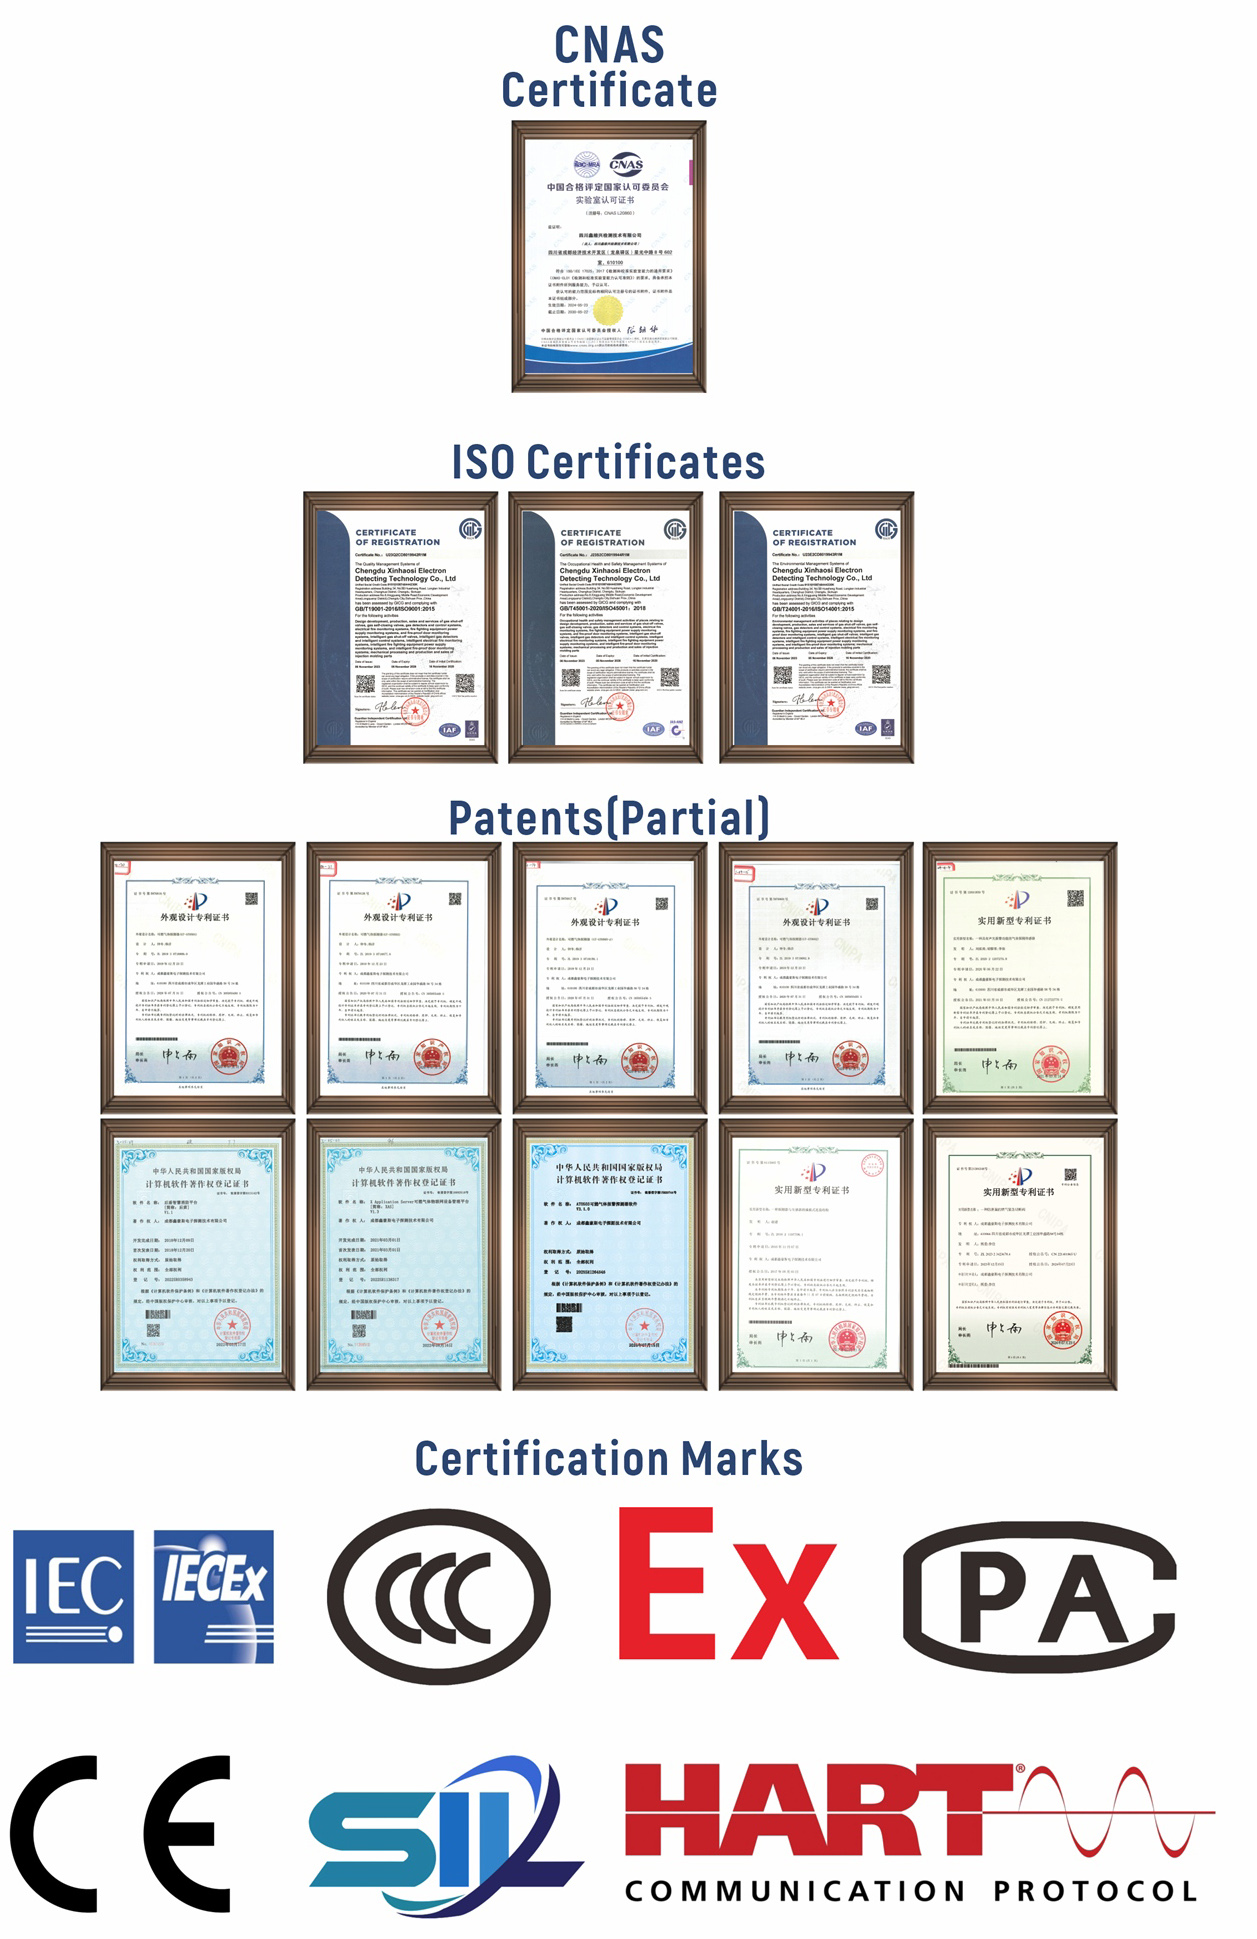
Adhering to ISO9001 quality management system standards, Xinhaosi's core products have obtained a full range of authoritative certifications, including national compulsory Products Certification, explosion-proof certification, fire product certification, CPA measurement instrument type approval certificate, and internatinal approvals as CE, SIL. Additionally, Xinhaosi holds honors such as "National Quality Integrity Benchmark Enterprise" , "National Quality Leading Enterprise in the Gas Alarm Industry," member of the China Fire Protection Association, and the main drafting organization for the national standard of solenoid valves, further confirming its industry influence and reputation.
In the field of intellectual property, Xinhaosi has built a robust innovation system with over 50 patents and software copyrights . These patents cover core technological areas, including a graphical monitoring system for gas detection and alarm, which enables predictive maintenance based on historical data to reduce equipment failure rates by over 30%, and a solenoid valve with flow monitoring functionality that integrates flow detection and alarm capabilities . The company also pioneered China's first networked bus-type gas leakage monitoring system and the only maximum-point gas leakage monitoring system certified by the Ministry of Public Security, demonstrating its leading position in cutting-edge technological research.
Our in-house laboratory is accredited by the China National Accreditation Service for Conformity Assessment (CNAS), recognized both domestically and internationally under the ILAC-MRA framework. It operates in accordance with ISO/IEC 17025, the international standard for testing and calibration laboratories. It provides reliable and traceable testing services for gas detection and alarm products, solenoid valves, and related safety equipment. Test reports issued by the CNAS-accredited laboratory are widely accepted by regulatory authorities, certification bodies, and customers in China and overseas, helping to ensure product quality, safety compliance, and market access.