Heavy-Duty Fixed Combustible & Toxic Gas Monitoring Systems Engineered for Solomon Islands Industrial Facilities
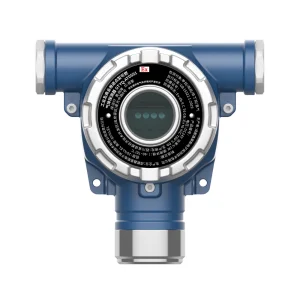
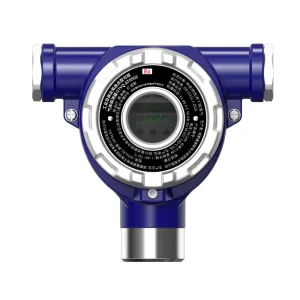
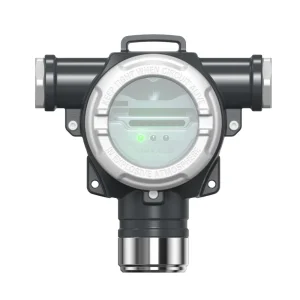
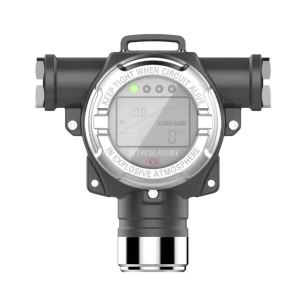
Bridging High-Risk Marine Operations and Tropical Processing Infrastructure with Precision Sensing
As the economic centerpiece of the Western Province in the Solomon Islands, Noro represents a vital hub for deep-sea tuna harvesting, commercial fish processing (SolTuna), bulk fuel marine bunkering, and active port logistics. The localized environment presents extreme microclimatic challenges: sustained relative humidity exceeding 85%, continuous marine salt-spray aerosol exposure (C5-M atmospheric corrosive classification), and ambient thermal stress. Fixed-type gas detection deployments in Noro demand uncompromising physical casing integrity, hydro-phobic membrane barriers, anti-poisoning sensor chemistry, and zero-drift calibration stability to protect cold-storage anhydrous ammonia ($NH_3$) facilities, power generation diesel storage, and municipal wastewater treatment assets.
Globally, industrial processing sectors are rapidly pivoting from reactive standalone gas buzzers toward integrated, cloud-connected SIL2/SIL3 safety instrumented systems (SIS). Modern manufacturing guidelines demand real-time data streaming over 4-20mA HART, RS485 Modbus, and wireless mesh topologies. Furthermore, stringent environmental mandates require fixed gas monitors to possess information-gain analytics—enabling predictive sensor degradation notifications, early leak plume triangulation, and automated emergency shutoff valve actuation. Gas Safety Pro delivers this global standard directly to emerging industrial centers like Noro.
Standard commercial-grade gas detectors frequently fail within 6 to 12 months in tropical island ports due to severe humidity condensation and salt crystallization over sensor diffusion windows. Our custom-configured fixed gas detectors incorporate dual-stage sintered stainless steel flame arrestors, internal silicone heating elements to prevent dew condensation, and anti-corrosive ADC12 die-cast aluminum or 316L stainless steel enclosures engineered specifically for maritime regions.
Advanced Sensor Physics Matched with Robust Explosion-Proof Engineering
Designed for long-term combustible gas monitoring ($CH_4$, $C_3H_8$) without risk of sensor poisoning from silicones or sulfur compounds. NDIR technology utilizes dual-wavelength optic channels to guarantee zero-point stability across variable island temperatures.
High-sensitivity detection for lower explosive limits (0-100% LEL) of flammable hydrocarbons. Built with heavy-duty catalytic elements engineered with poison-resistant coatings, ideal for fuel terminal pump houses and generator rooms.
Ultra-precise toxic gas detection ($NH_3$, $H_2S$, $CO$, $Cl_2$) down to parts-per-million (PPM) thresholds. Features specialized electrolyte gels that resist dehydration under high tropical heat ambient profiles.
Turnkey Safety Engineering for Cannery Processing, Bunkering Ports, and Utilities
Anhydrous Ammonia ($NH_3$) refrigeration systems require continuous zero-drift sensing. Our fixed monitors integrate fast T90 response times, triggering localized multi-tone sirens and automatic emergency exhaust louvers long before toxic thresholds pose operator hazards.
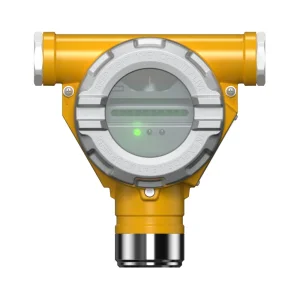
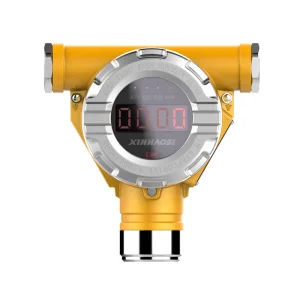
Noro Port’s marine bunkering operations demand ATEX/IECEx Zone 1 certified flameproof gas transmitters. Integrated with explosion-proof cast enclosures, these units continuously scan for diesel fuel vapors, LPG, and volatile hydrocarbons.
Wastewater treatment installations and diesel-generator microgrids utilize our networked gas controllers. Featuring 4-20mA Modbus communication lines, gas alarms relay emergency trip signals straight to centralized monitoring rooms.
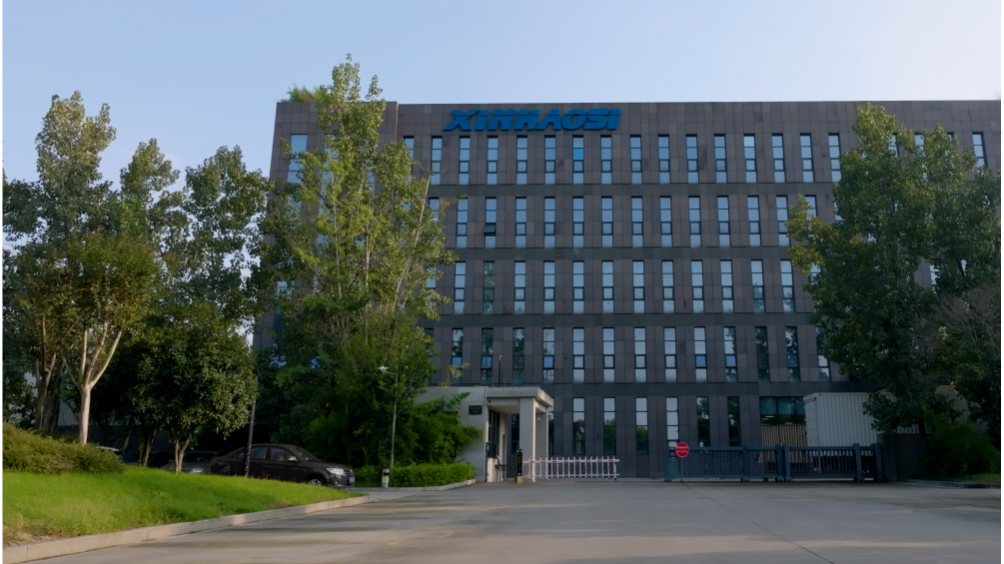
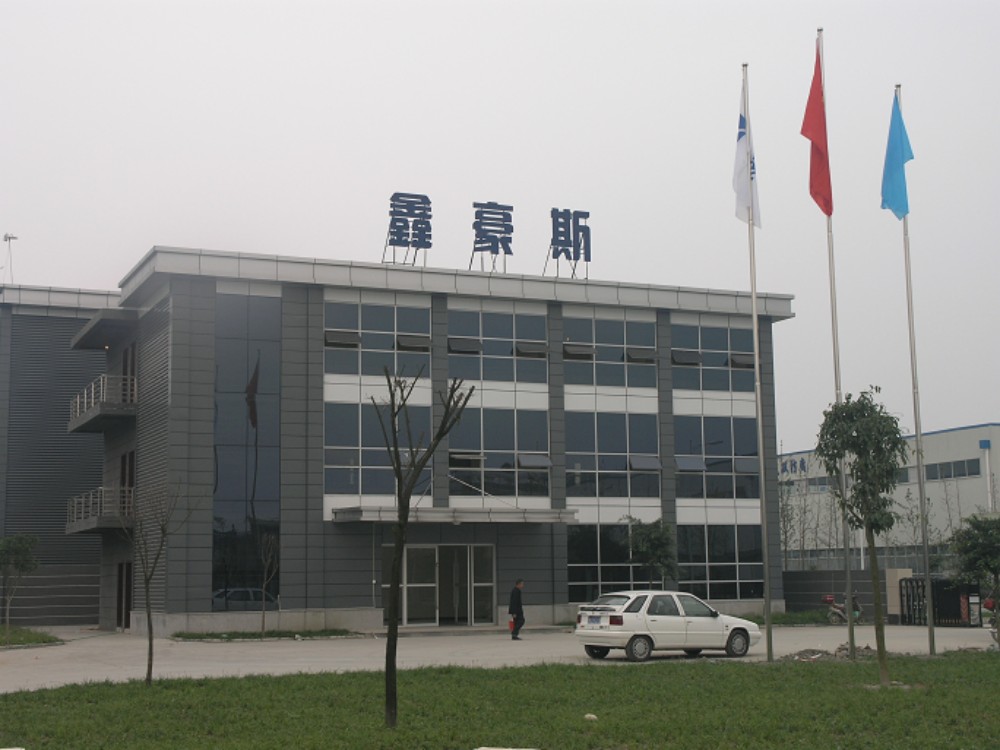
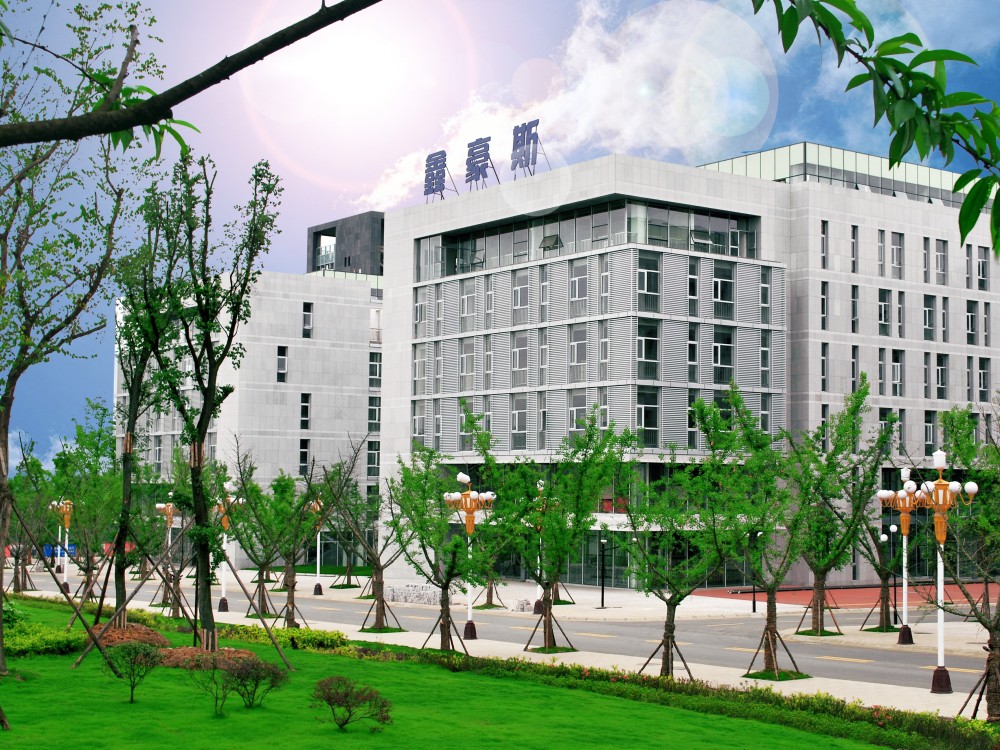
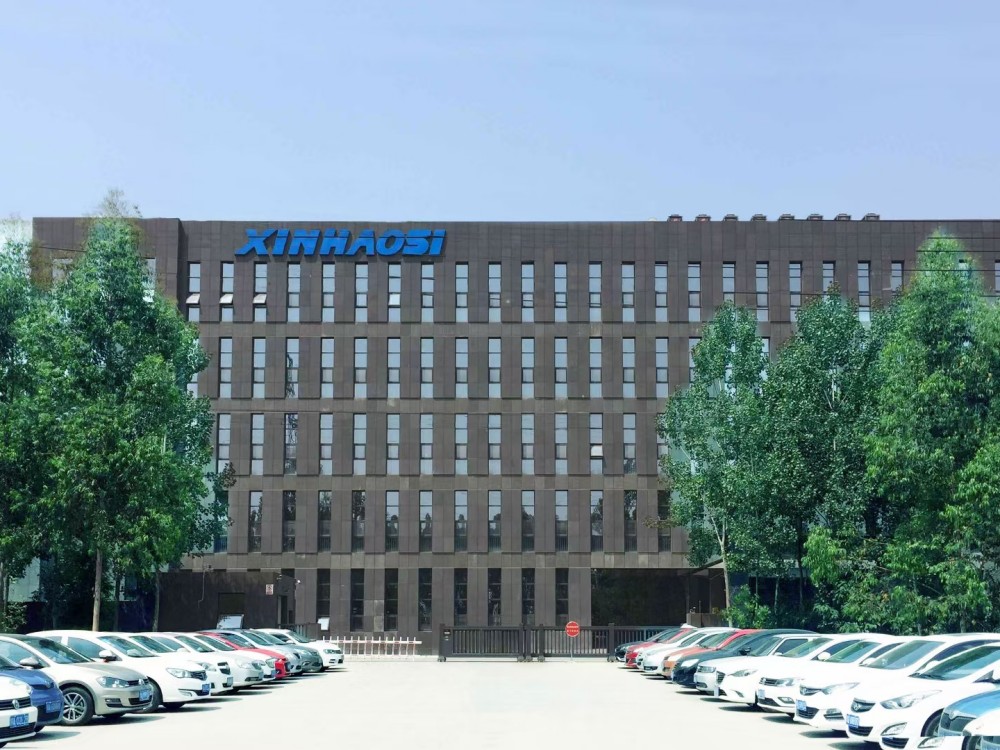
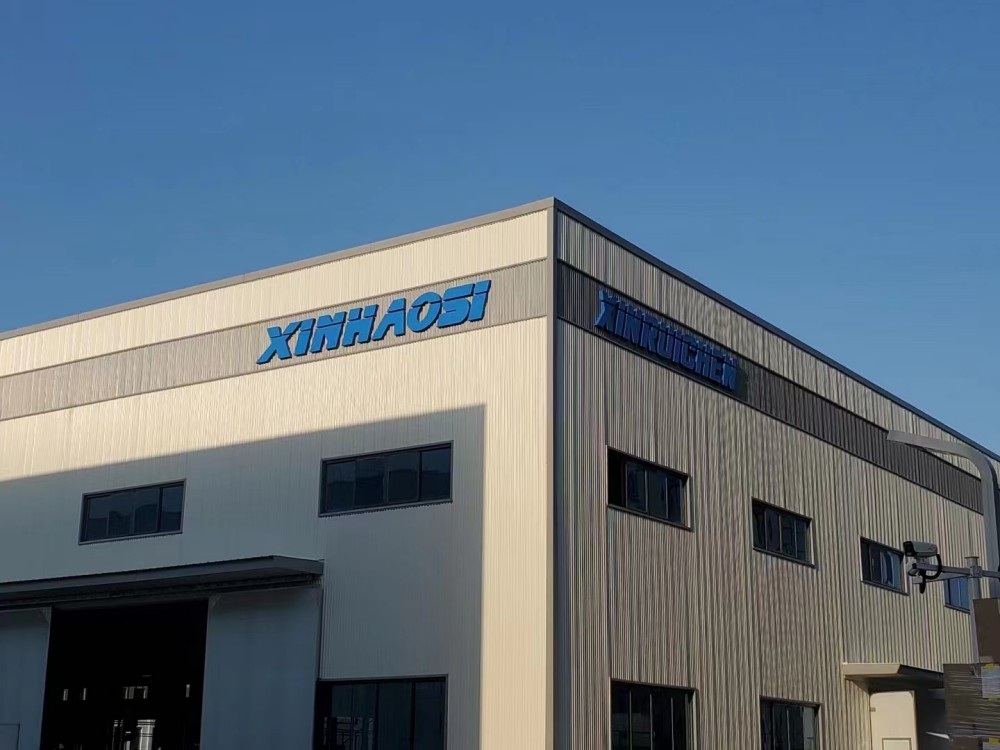
Chengdu Headquarter & R&D Center
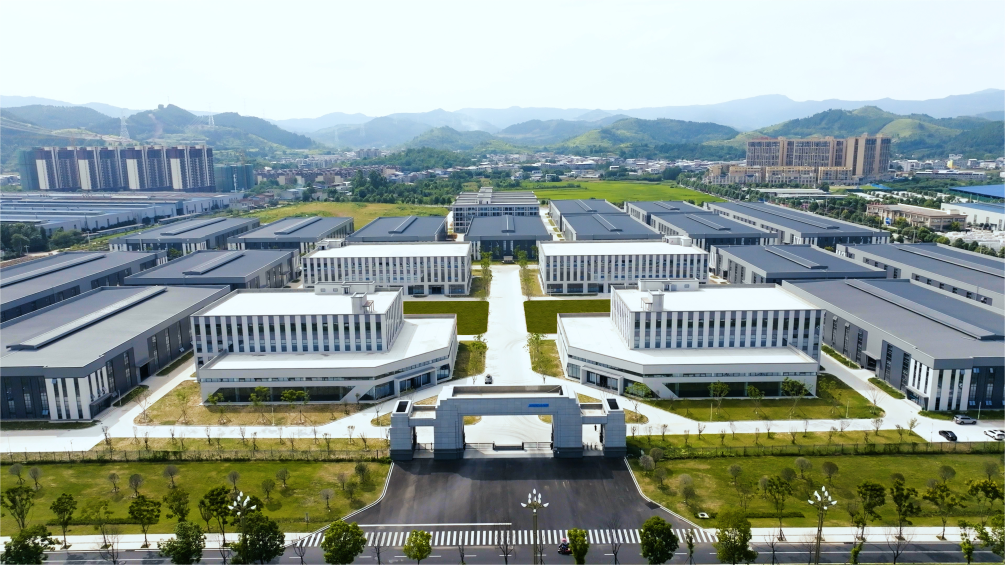
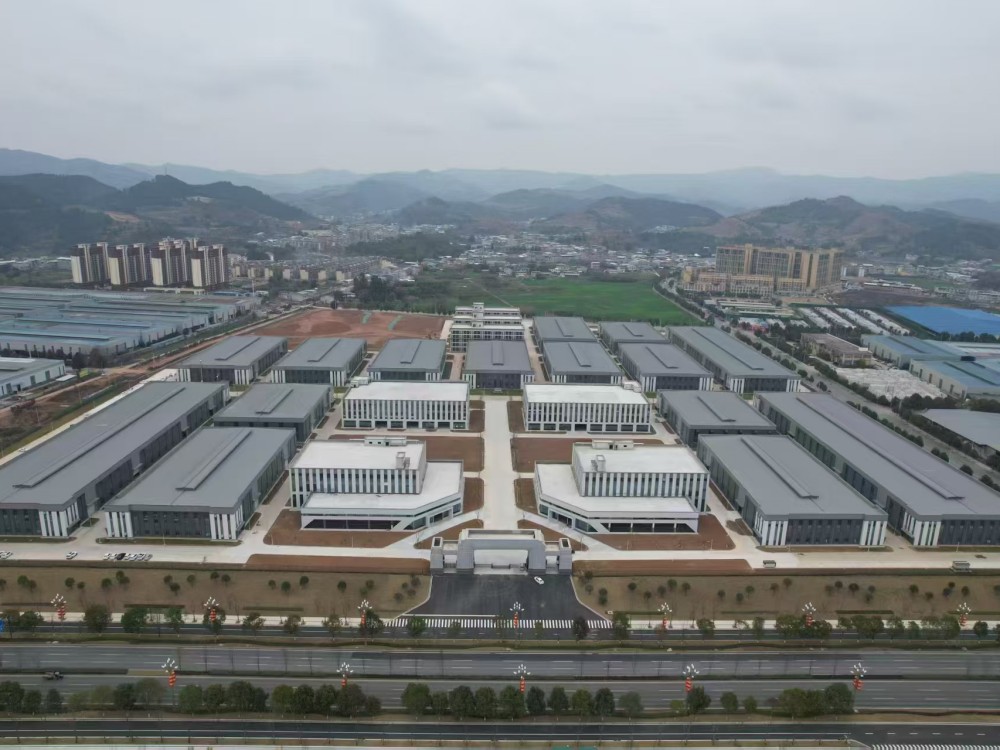
Deyang Intelligent Manufacturing Base
Founded in 2003, Xinhaosi is one of the most influential and trusted brands in the global gas safety industry. Over the past two decades, we have steadily built a robust and comprehensive production and service system, which integrates cutting-edge R&D, intelligent manufacturing with advanced automation equipment, digital marketing across global channels, professional after-sales support with an experienced technician team, flexible OEM/ODM services, as well as CNAS-Accredited laboratory calibration services that meet international standards.
Our diversified product portfolio covers industrial & residential gas detection & alarm systems, industrial & household gas solenoid valves, and urban gas pipeline network monitoring systems—all engineered to adapt to complex working environments and strict safety requirements. We produce and sell tens of millions of units annually, catering to a wide range of industries that demand reliable gas detection solutions, including oil & gas exploration and production, petrochemicals, urban gas distribution, automotive manufacturing, pharmaceuticals, new energy, steel production, and beverage processing.
Guided by the core mission of “Making Gas Safety Accessible Everywhere,” we consistently deliver high-performance, reliable products and customized solutions tailored to each client’s unique needs. Every item we manufacture undergoes rigorous quality control tests, and every service we provide is backed by our professional technical team, fully embodying our unwavering commitment to safeguarding gas safety across both industrial workplaces and residential environments, and striving to build a safer world with sustainable gas safety technologies.
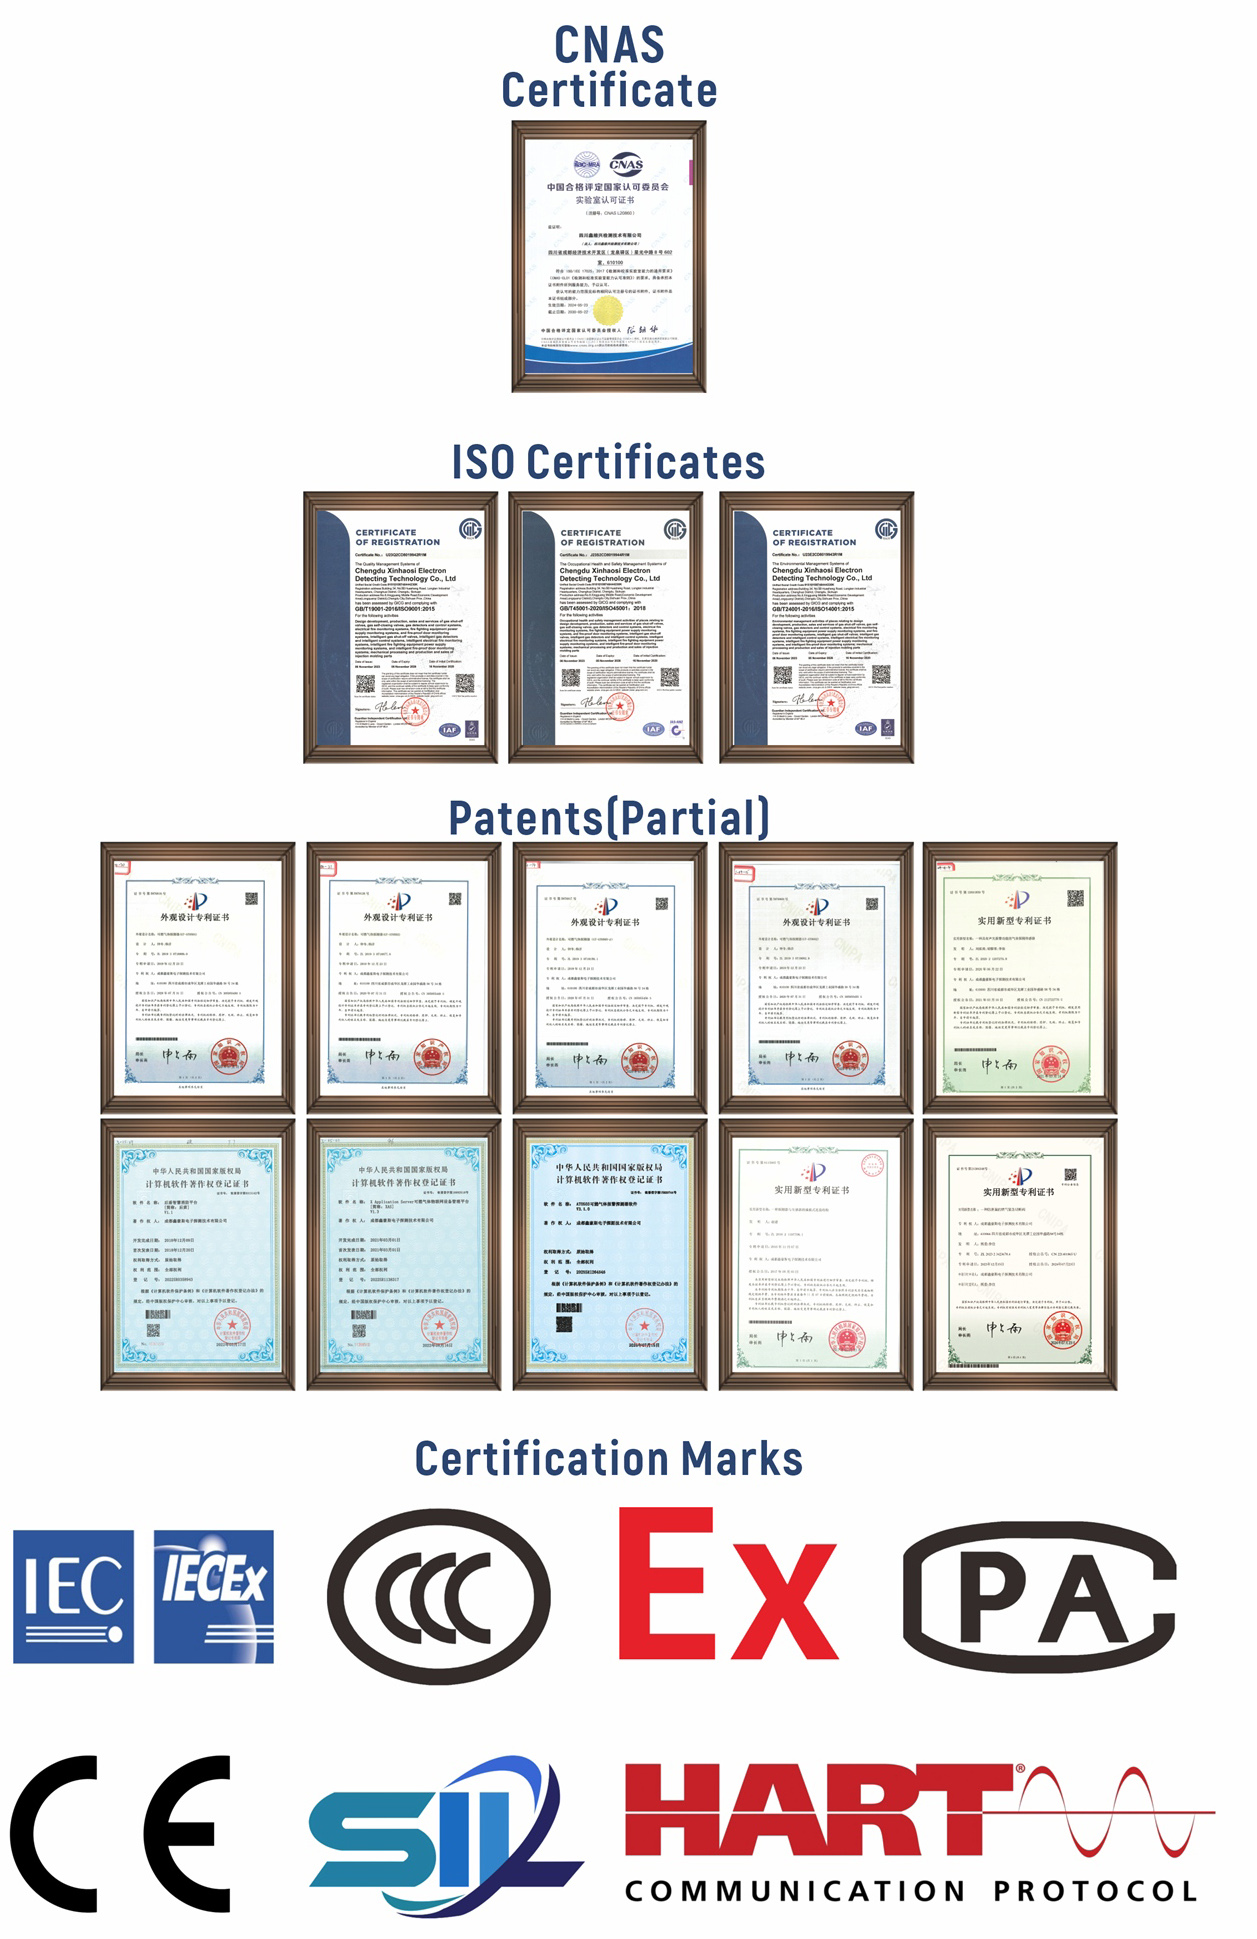
Adhering to ISO9001 quality management system standards, Xinhaosi's core products have obtained a full range of authoritative certifications, including national compulsory Products Certification, explosion-proof certification, fire product certification, CPA measurement instrument type approval certificate, and international approvals as CE, SIL. Additionally, Xinhaosi holds honors such as "National Quality Integrity Benchmark Enterprise" , "National Quality Leading Enterprise in the Gas Alarm Industry," member of the China Fire Protection Association, and the main drafting organization for the national standard of solenoid valves, further confirming its industry influence and reputation.
In the field of intellectual property, Xinhaosi has built a robust innovation system with over 50 patents and software copyrights . These patents cover core technological areas, including a graphical monitoring system for gas detection and alarm, which enables predictive maintenance based on historical data to reduce equipment failure rates by over 30%, and a solenoid valve with flow monitoring functionality that integrates flow detection and alarm capabilities . The company also pioneered China's first networked bus-type gas leakage monitoring system and the only maximum-point gas leakage monitoring system certified by the Ministry of Public Security, demonstrating its leading position in cutting-edge technological research.
Our in-house laboratory is accredited by the China National Accreditation Service for Conformity Assessment (CNAS), recognized both domestically and internationally under the ILAC-MRA framework. It operates in accordance with ISO/IEC 17025, the international standard for testing and calibration laboratories. It provides reliable and traceable testing services for gas detection and alarm products, solenoid valves, and related safety equipment. Test reports issued by the CNAS-accredited laboratory are widely accepted by regulatory authorities, certification bodies, and customers in China and overseas, helping to ensure product quality, safety compliance, and market access.
Two Decades of Continuous Innovation in Global Gas Safety Solutions
Expert Guidance on Installation, Calibration, and Maintenance for Noro Engineers
Explore Comprehensive Detection Models Engineered for Combustible, Toxic, Oxygen & VOC Hazards
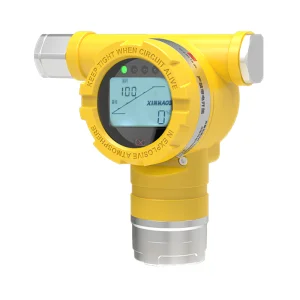
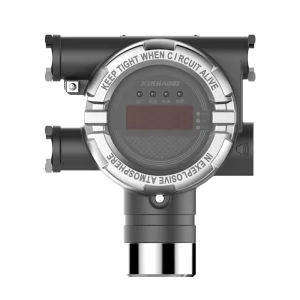
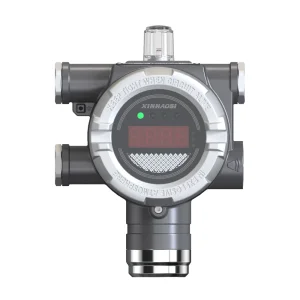
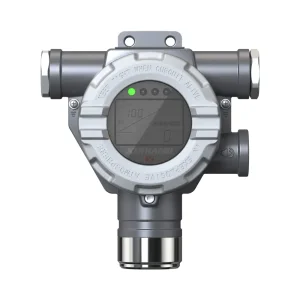
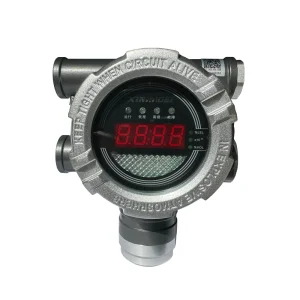
Partner directly with an established global manufacturer. Request customized engineering specifications, SIL certification documentation, or localized project quotes today.
Send Inquiry Now