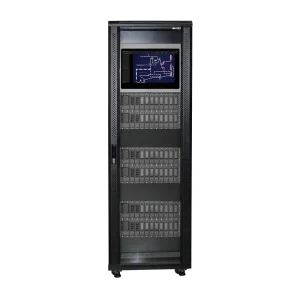
High-reliability centralized monitoring control units built to withstand sub-zero temperature operational windows, high vibration, and heavy dust environments in Mongolian industrial sites.
Designed for heavy industrial installations in Erdenet. Features multi-bus channel capacity, rapid alarm response, and Modbus RTU integration.
View Technical Details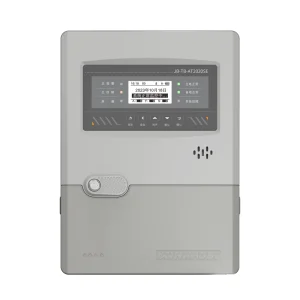
Compact wall-mounted industrial controller tailored for Erdenet copper-molybdenum concentration plants and thermal energy units.
View Technical Details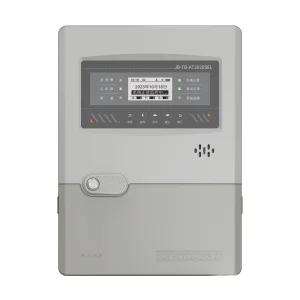
High-capacity multi-loop control console featuring LCD status visualizers and automated solenoid valve interlock capabilities for mining safety.
View Technical Details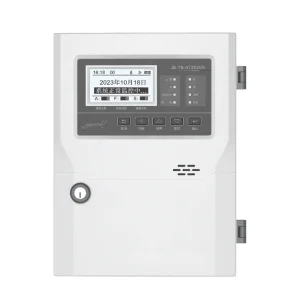
Modular gas safety controller engineered with low-temperature tolerance components, optimal for underground shafts and complex chemical complexes.
View Technical DetailsErdenet, the third-largest city in Mongolia and the capital of Orkhon Province, represents one of Asia's premier industrial hubs centered on copper and molybdenum mining, mineral processing, and thermal power production.
The operations of major industrial complexes—most notably the Erdenet Mining Corporation (EMC), associated copper leaching plants, and regional thermal energy infrastructure—demand continuous, non-interrupted gas monitoring. Hazardous industrial gases including Sulfur Dioxide ($\text{SO}_2$), Hydrogen Sulfide ($\text{H}_2\text{S}$), Carbon Monoxide ($\text{CO}$), and explosive gases such as Methane ($\text{CH}_4$) present catastrophic risks to personnel and heavy capital equipment if undetected.
Sub-Arctic Environmental Resilience: In Erdenet's extreme continental climate, winter temperatures drop to below -40°C. Gas detector controllers must feature wide operational temperature limits, drift compensation algorithms, and heavy-duty dust protection (IP66/IP67) to prevent thermal lockup or false alarms.
Erdenet's large-scale copper-molybdenum concentration processes involve flotation reagents, chemical leaching tanks, and heavy mechanical crushing. Multi-channel gas controllers aggregate real-time telemetry from hazardous zones to safeguard workers against toxic reagent off-gassing and $\text{H}_2\text{S}$ buildup.
Coal-fired boilers and industrial power houses in Orkhon Province produce high concentrations of $\text{CO}$ and potential combustible gas leaks. Centralized controllers automatically initiate exhaust fan ventilation and actuate emergency gas shutoff valves upon detecting toxic threshold breaches.
Beyond heavy mining, Erdenet's expanding municipal gas pipelines, commercial boiler houses, and residential neighborhoods require standardized combustible gas detection systems and automatic wireless cut-off solenoid valves to guarantee community safety.
Our enterprise-grade Gas Detector Controllers utilize advanced bus communication topologies, modular expansion hardware, and cloud IoT connectivity to deliver unmatched reliability for high-density sensor networks.
The JB-TB-AT2020 series gas detector controllers utilize dual non-polar M-Bus two-wire communication and RS485 Modbus-RTU protocols. This enables long-distance signal transmission (up to 1,200 meters without signal repeaters) across expansive mining facilities in Erdenet, significantly reducing wiring costs and installation complexity.
Equipped with customizable relay outputs, the controller can seamlessly interface with external safety equipment. Upon detecting elevated gas concentrations, the system automatically triggers:
Founded in 2003, Xinhaosi has established itself as an authoritative global leader in industrial gas monitoring, serving industrial clients across Asia, Europe, and America.
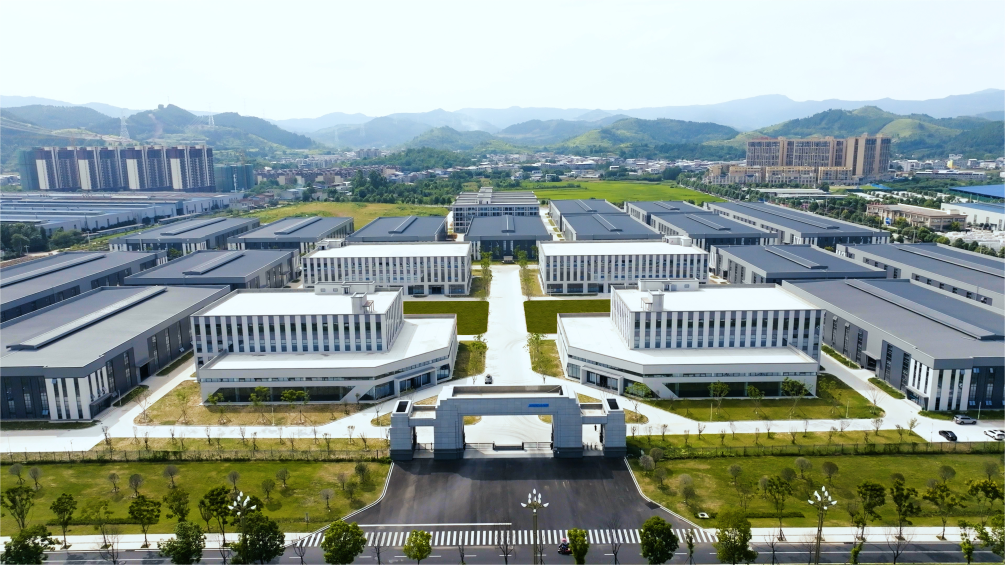
Operating dual state-of-the-art intelligent manufacturing bases in Chengdu and Deyang, our facilities feature automated Surface Mount Technology (SMT) production lines, computerized calibration stations, and digital quality management platforms. We produce tens of millions of detection units and safety control valves annually, supplying world-leading energy companies and municipal gas suppliers.
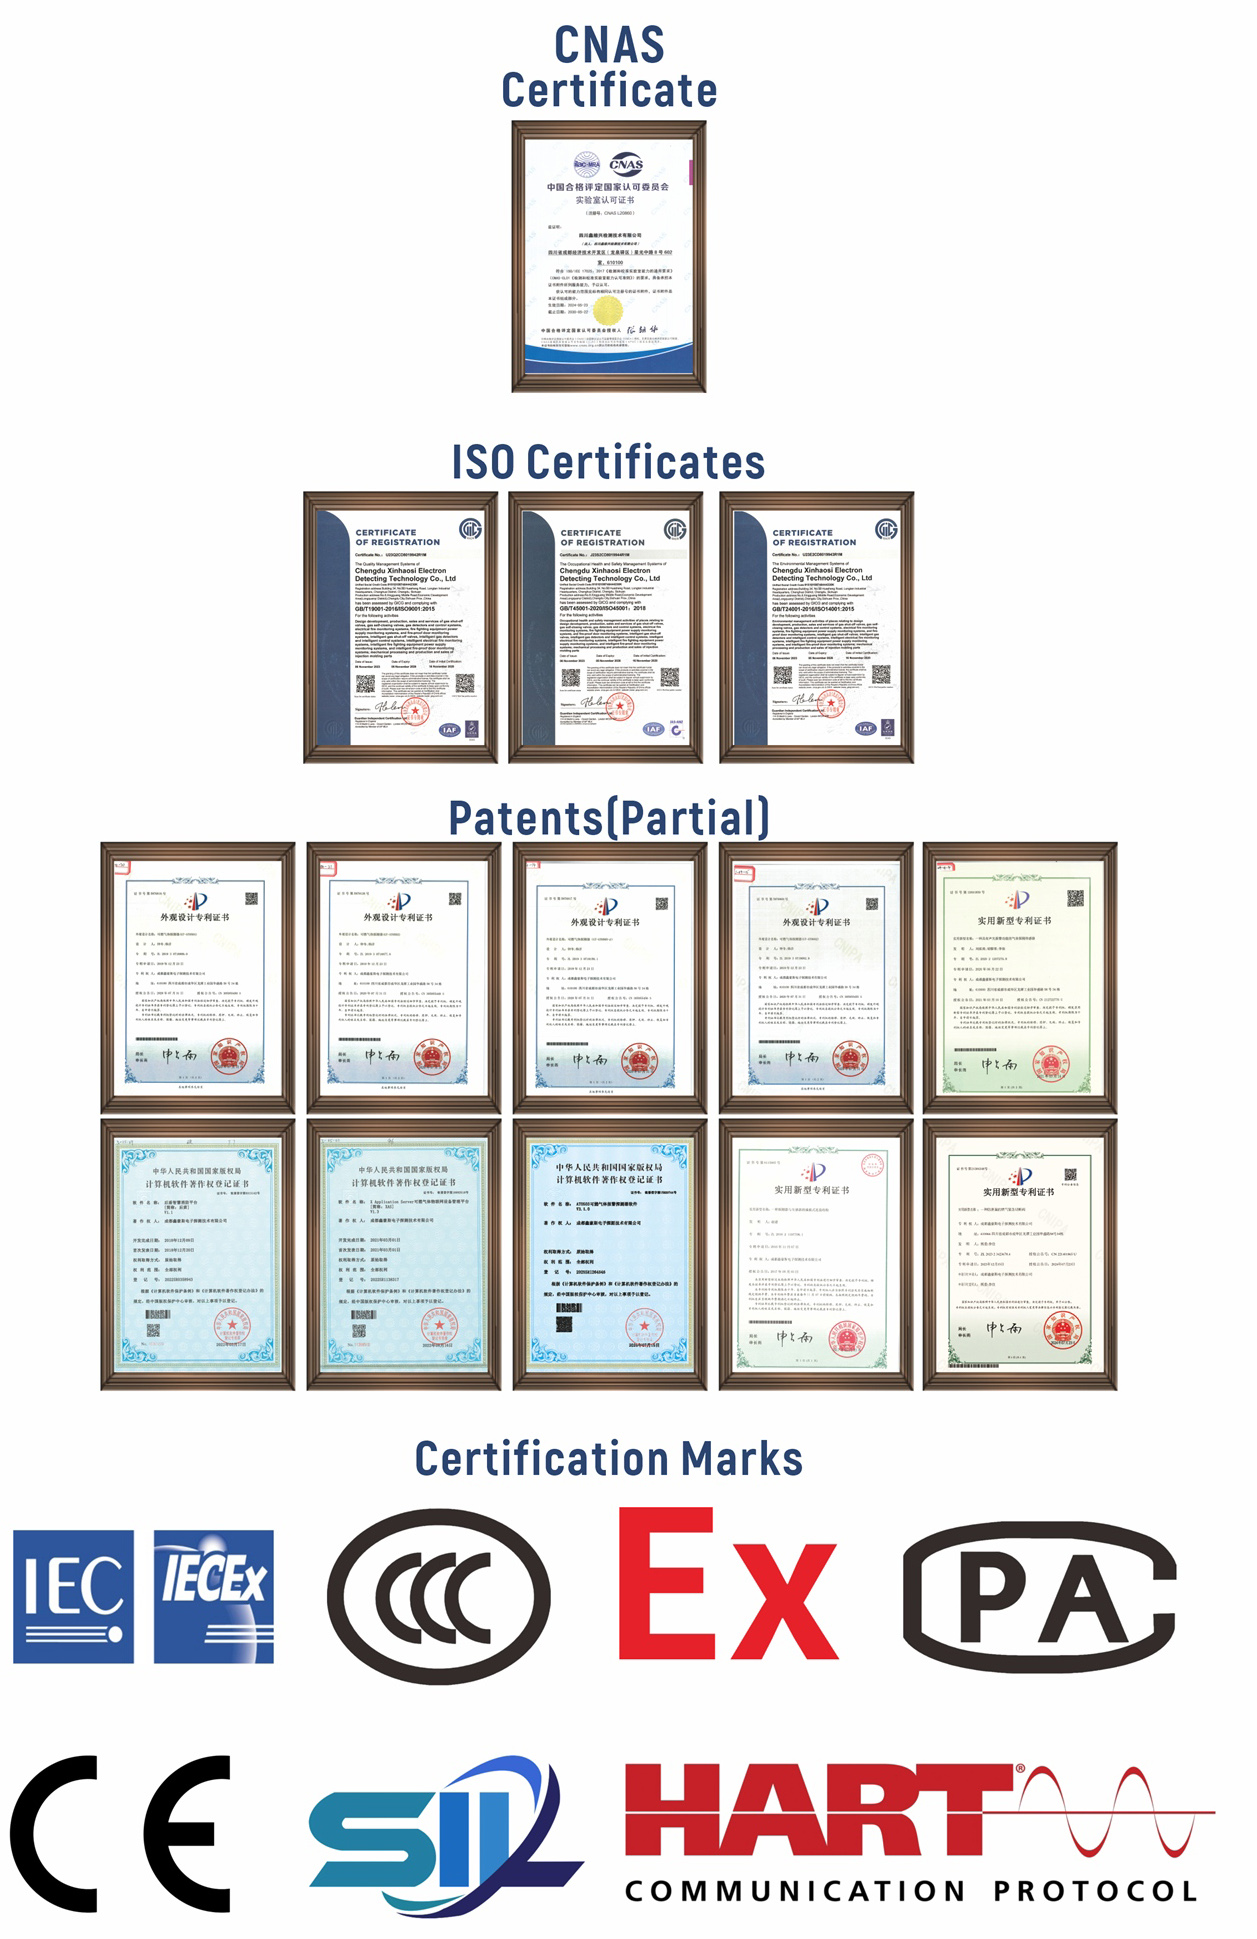
Our in-house calibration and testing laboratory is accredited by the China National Accreditation Service for Conformity Assessment (CNAS), operating under the international ISO/IEC 17025 standard and recognized globally via the ILAC-MRA framework. Test reports issued by our CNAS laboratory are accepted by international regulatory bodies, certifying product performance under harsh thermal, vibration, and chemical stress environments.
Holding over 50 patents and software copyrights, Xinhaosi pioneered China's first networked bus-type gas leakage monitoring platform and graphical software predictive maintenance system—reducing plant equipment failure rates by over 30%. Our products hold full ISO9001, SIL2, SIL3, CE, CPA (Measurement Approval), and explosion-proof (Ex d IIC T6) certifications.
Explore our complete lineup of certified explosion-proof gas detectors, input/output interface modules, low-voltage power supply boxes, and automatic shutoff valves designed for Erdenet's industrial spectrum.
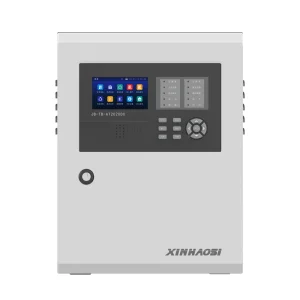
Heavy-duty industrial control panel engineered for dense sensor networks in metal processing plants.
Product Specifications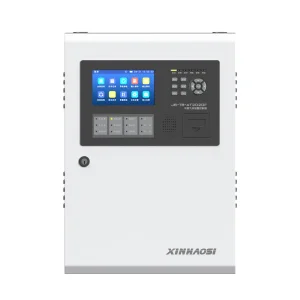
Fire protection certified gas monitoring controller for industrial boiler rooms and power facilities.
Product Specifications
Modular multi-channel bus panel with high anti-interference circuitry against mining heavy machinery EMI.
Product Specifications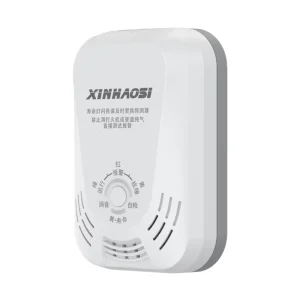
Precision residential combustible gas detector featuring high sensitivity sensors and automatic valve linkage.
Product Specifications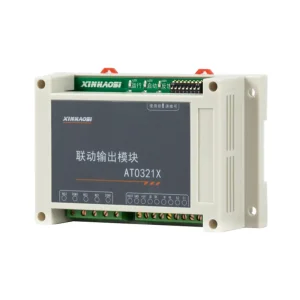
Bus-type relay output interface modules for switching high-current exhaust fans and industrial shut-off valves.
Product Specifications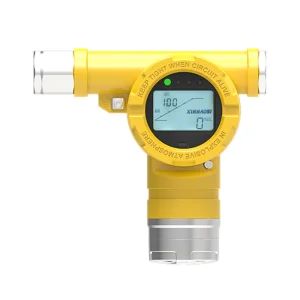
ATEX/IECEx certified Ex d IIC T6 gas detector head built for hazardous chemical and copper leaching environments.
Product Specifications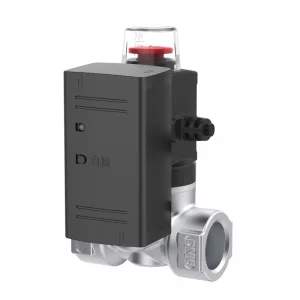
Ultra-low power wireless gas shut-off valve designed for convenient domestic utility safety retrofits.
Product Specifications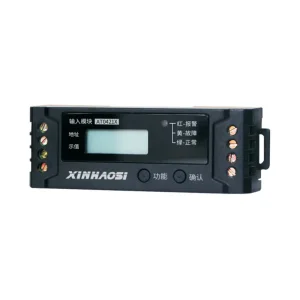
Bus input monitoring unit for converting standard 4-20mA analog sensor signals into digitally networked telemetry.
Product Specifications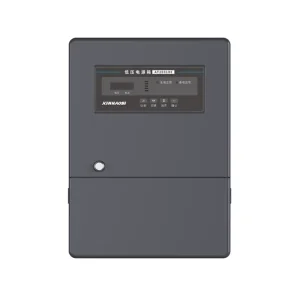
Redundant power supply station ensuring continuous controller operation during power fluctuations in remote industrial zones.
Product Specifications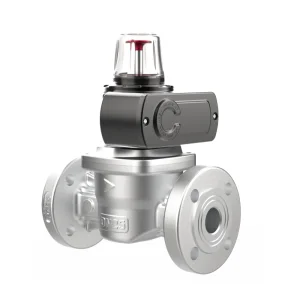
High-pressure normally open industrial shut-off valve designed for quick emergency isolation of major gas pipelines.
Product Specifications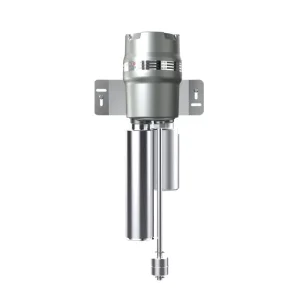
Specialized underground shaft monitoring unit optimized for mining tunnels, pit shafts, and confined spaces.
Product Specifications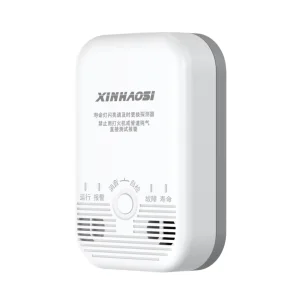
Advanced residential gas monitoring detector with dual sensor technology and wireless hub integration.
Product SpecificationsDeploying gas monitoring hardware in Orkhon Province requires strict alignment with local safety mandates, Mongolian National Standards (MNS), and harsh-weather engineering specifications.
Standard gas controllers often suffer from LCD freezing, power supply voltage drops, and sensor zero-point drift under extreme freeze conditions (-30°C to -45°C). Xinhaosi gas detector controllers integrate wide-temperature grade components, internal thermostatic heating options, and automatic temperature compensation software.
We provide full OEM/ODM engineering services to engineering contractors and industrial plant operators across Erdenet. Customization options include:
As Erdenet's industrial facilities modernize toward Industry 4.0 standards, gas safety systems are transitioning from passive emergency alarms to proactive AI predictive maintenance networks.
By analyzing historical telemetry data, our AI algorithms predict sensor degradation and zero-point drift before hardware failure occurs, allowing plant engineers to schedule maintenance without unexpected downtime.
Eliminating physical cabling in complex outdoor tailing ponds and open-pit mining perimeters. Battery-operated wireless nodes transmit real-time gas telemetry directly to central controllers.
Next-generation AI valves equipped with internal flow rate monitoring, self-testing solenoid coils, and instant automatic closure in sub-second timeframes during seismic or gas rupture events.
Detailed engineering answers to address procurement, technical integration, and operational queries in Orkhon Province, Mongolia.
Our industrial controllers (such as the JB-TB-AT2020 series) are manufactured using industrial-grade electronic components rated for extended ambient temperature ranges. For extreme outdoor or unheated panel installations, we supply custom enclosure options equipped with internal thermostatic heating elements and wide-temperature OLED/LCD screens to prevent freeze-up.
Our gas detector controllers support standard industrial RS485 Modbus-RTU, non-polar M-Bus, and 4-20mA current loops. Additionally, optional Ethernet interfaces and cloud IoT gateways allow seamless data transfer into centralized plant platforms like Siemens PCS7, ABB Ability, or Honeywell Experion DCS.
Yes. The JB-TB-AT2020 series multi-channel controllers dynamically address and manage mixed sensor arrays. A single bus loop can simultaneously poll toxic gas detector heads ($\text{SO}_2, \text{H}_2\text{S}, \text{CO}$), oxygen depletion sensors, and catalytic or infrared combustible gas detectors ($\text{CH}_4, \text{LPG}$).
Our industrial gas detector heads (such as the XP3000 series) hold Ex d IIC T6 Gb explosion-proof certification, ATEX, IECEx, and China National Explosion-Proof standards. Central controllers are rated for safe area wall mounting or housed within Ex d flameproof enclosures for hazardous zone placement.
Utilizing our non-polar M-Bus two-wire topology or RS485 shielded twisted-pair cabling (2x1.5mm²), transmission distances up to 1,200 meters are achieved without signal degradation. For longer distances across mining concessions, fiber optic converters or wireless mesh gateways are integrated.
Our control cabinets feature integrated standby battery management circuits and automatically link with low-voltage auxiliary power boxes like the AT2031XE. Upon AC mains interruption, the system seamlessly switches to internal DC backup batteries for up to 24+ hours of uninterrupted operation.
Yes. All gas detector controllers and sensor heads undergo factory calibration in our CNAS-accredited laboratory (ISO/IEC 17025 compliant). Each shipment is supplied with individual calibration certificates traceable to national measurement standards.
Standard controller and detector models are dispatched from our Deyang/Chengdu logistics hubs within 7-14 business days. Customized OEM/ODM solutions tailored for major mining projects typically ship within 3 to 4 weeks via direct rail or overland transport to Mongolia.
Partner with an established global manufacturer of SIL2-certified Gas Detector Controllers, Safety Valves, and Remote Telemetry Systems. Request technical specifications, CAD schematics, or factory-direct quotations.
Send Inquiry Now